English - EN
 繁體 - ZH-TW
 简体 - ZH-CN
 Español - ES
 日本語 - JA
 العربية - AR
 Русский - RU
 Français - FR

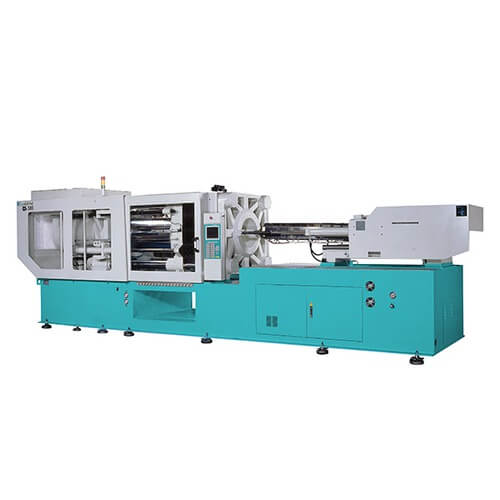
Classification: Hydraulic Clamping Injection Molding Machines

| Item | Unit | CI-300 | CI-300S | CI-400 | |||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| SCREM DIA | mm | 50 | 56 | 63 | 70 | 45 | 50 | 56 | 63 | 56 | 63 | 70 | 80 |
| INJ. VOLUME | cm3/shot | 490 | 615 | 779 | 962 | 358 | 441 | 554 | 701 | 690 | 872 | 1077 | 1407 |
| INJ. CAPACITY | g | 466 | 584 | 740 | 914 | 340 | 419 | 526 | 666 | 656 | 829 | 1023 | 1336 |
| PLASTICIZING RATE | kg/hr(ps) | 97 | 125 | 167 | 285 | 77 | 97 | 131 | 183 | 130 | 162 | 228 | 317 |
| INJ. PRESS | kgf/cm2 | 2463 | 1964 | 1552 | 1256 | 2500 | 2023 | 1612 | 1274 | 2460 | 1945 | 1575 | 1205 |
| INJ. RATE | cm3/sec | 267 | 335 | 424 | 523 | 243 | 300 | 377 | 477 | 337 | 426 | 527 | 688 |
| INJ. STROKE | mm | 250 | 225 | 200 | |||||||||
| INJ. SPEED | mm/s | 136 | 153 | 165 | |||||||||
| SCREW SPEED | rpm | 0~270 | 0~310 | 0~310 | |||||||||
| NOZZLE STROKE | mm | 430 | 380 | 330 | |||||||||
| NOZZLE FORCE | tonf | 6.8 | 6.8 | 4.2 | |||||||||
| CLAMP FORCE | tonf | 300 | 300 | 200 | |||||||||
| CLAMP STROKE | mm | 850 | 850 | 700 | |||||||||
| MIN. THICKNESS | mm | 300 | 300 | 250 | |||||||||
| DAYLIGHT OPEN | mm | 1150 | 1150 | 950 | |||||||||
| TIE BAR DISTANCE | mm | 660*660 | 660*660 | 530*530 | |||||||||
| PLATEN SIZE | mm | 955*955 | 955*955 | 770*770 | |||||||||
| EJECTOR STROKE | mm | 130 | 130 | 110 | |||||||||
| EJECTOR FORCE | tonf(kN) | 9.6 | 9.6 | 7.7 | |||||||||
| OPINING FORCE | tonf(kN) | 12 | 12 | 9 | |||||||||
| MAX. SYS. PRESS | kgf/cm2 | 170 | 170 | 170 | |||||||||
| MOTOR POWER | kw(hp) | 37(50) | 37(50) | 30(40) | |||||||||
| HEATER CAPACITY | kw | 17 | 16 | 13.7 | |||||||||
| HYD. OIL REQ | L | 950 | 950 | 660 | |||||||||
| MACHINE DIMESIONS(L*W*H) | M | 6*1.5*2 | 6*1.5*2 | 5.6*1.3*1.9 | |||||||||
| FLOOR SPACE | M | 5.6*1.4 | 5.6*1.4 | 4.8*1.2 | |||||||||
| MACHINE WEIGHT | ton | 12.5 | 12 | 7.4 | |||||||||
| Item | Unit | CI-400S | CI-500 | CI-500S | |||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| SCREM DIA | mm | 50 | 56 | 63 | 70 | 63 | 70 | 80 | 90 | 56 | 63 | 70 | 80 |
| INJ. VOLUME | cm3/shot | 490 | 615 | 779 | 962 | 997 | 1231 | 1608 | 2035 | 251 | 318 | 392 | 492 |
| INJ. CAPACITY | g | 466 | 584 | 740 | 914 | 947 | 1169 | 1527 | 1933 | 238 | 302 | 372 | 467 |
| PLASTICIZING RATE | kg/hr(ps) | 97 | 125 | 167 | 235 | 150 | 200 | 274 | 380 | 66 | 72 | 98 | 134 |
| INJ. PRESS | kgf/cm2 | 2463 | 1964 | 1552 | 1256 | 2470 | 2000 | 1531 | 1209 | 2626 | 2076 | 1681 | 1340 |
| INJ. RATE | cm3/sec | 333 | 418 | 529 | 654 | 343 | 424 | 553 | 700 | 251 | 318 | 392 | 492 |
| INJ. STROKE | mm | 175 | 320 | 280 | |||||||||
| INJ. SPEED | mm/s | 188 | 110 | 140 | |||||||||
| SCREW SPEED | rpm | 0~410 | 0~157 | 0~200 | |||||||||
| NOZZLE STROKE | mm | 320 | 520 | 470 | |||||||||
| NOZZLE FORCE | tonf | 4.2 | 12 | 8.8 | |||||||||
| CLAMP FORCE | tonf | 200 | 500 | 500 | |||||||||
| CLAMP STROKE | mm | 700 | 1050 | 1050 | |||||||||
| MIN. THICKNESS | mm | 250 | 350 | 350 | |||||||||
| DAYLIGHT OPEN | mm | 950 | 1400 | 1400 | |||||||||
| TIE BAR DISTANCE | mm | 530*530 | 820*820 | 820820 | |||||||||
| PLATEN SIZE | mm | 770*770 | 1190*1190 | 1190*1190 | |||||||||
| EJECTOR STROKE | mm | 110 | 160 | 160 | |||||||||
| EJECTOR FORCE | tonf(kN) | 7.7 | 12 | 12 | |||||||||
| OPINING FORCE | tonf(kN) | 9 | 15 | 15 | |||||||||
| MAX. SYS. PRESS | kgf/cm2 | 170 | 170 | 170 | |||||||||
| MOTOR POWER | kw(hp) | 30(40) | 45(60) | 45(60) | |||||||||
| HEATER CAPACITY | kw | 10.3 | 28 | 25 | |||||||||
| HYD. OIL REQ | L | 660 | 1500 | 1500 | |||||||||
| MACHINE DIMESIONS(L*W*H) | M | 5.6*1.3*1.9 | 7.6*1.8*2.3 | 7.6*1.8*2.3 | |||||||||
| FLOOR SPACE | M | 4.8*1.2 | 6.9*1.6 | 6.9*1.6 | |||||||||
| MACHINE WEIGHT | ton | 7.1 | 20 | 19.3 | |||||||||
Clamping Unit:

Hydraulic clamping makes high-quality production
- The clamp distributes the pressure evenly. used for long- term, it will never be twisted. The tiebars are fixed securely and will always rem ain perfectly parallel. Due tathe fie bar special design, the mold can move very smoothly with vitually little friction, causing minimal stress or wear on the bars on the molding.
- The fast cylinder goes with the mold into the low-pressure.
Injection Unit:

High ability of plasticizing, High quality, High-speed molding
- The injection cylinder can rotate as well as move linearly, So there is very little friction and wear. It can be operated very stable and quietly. With this machine, high-speed molding is yours.
- Adjust back pressure with control of computer numericd unit.
- The operator can make fine funed odjustments.
- CI-250,CI-300 adopt double cylinder design to shorten machine length.
 |
 |
Single injection cylinder |
Dual injection cylinder |

Energy-saving means money-saving(option)
The energy-saving pump meets pollution requirements. It works quietly and requires only 60% of the energy needed by fraditiond pumps.

Hydraulic unit:
Short-term cycle
The oil tank is bosed on a brand-new design concept to apply oil to the cylinder for very high-speed mavement, dlowing a very fast production cycle.
Injection compression:
Low-pressure, In-mold compression, Low twist

Clamping
- Direct hydraulic damping
- True parallelism between tie bars, high precision in find products
- Strong platen, constrain is minimized
- Clamping for ce is evenly distibuted
- Improved tie bar spacing to acccpt larger molds
- Fix two end points, maintain tie bar parallelism
- Special tie bar structure design, reduce central constroin.
- High speed Oil tank.
- Oil supply with minimum friction.
Injection
- Injection compression for thin wall products
- Injection, storage
- 2nd charge function enable bigger capacity.
- 4 phose injection, 3 phose pressure cssure (changeable to 5 injection, 2 pressure)
- 3 phose charge.
- Auto purge.
- Injection end pont setup
- Cold start protection.
- Injection end point curve, injection precision statistic curve.
- Display injection precision.
- Single cylinder injection and charge motor in same axis.
- Low injection & charge friction.
- Low friction between barrdl & screw enable best transparent plastic injection.
- Low noise.
- Energy saving pump, full utilization of energy, save up to 40%* opion*
Controller
- Programmable "STAR" controller, made in Japan.
- High resalution display screen with various function display.
- SPC parameter is easy to set up & modify.
- Monitor operation procedure.
- Instart display operation & operation time.
- Open, close mode & ejection.
- Production management.
- 4 steps temperature setup, expand to 6 steps.
- Oil temperature display in 1 section.
- Oil prehcat function.
- Thermo control curve.
- 100 SPC recard.
- SPC precision comparison.
- Internal storage of 60 machine setup.
- Display temperature predision scale.
- Pressure curve*, Speedcurve*.
- IC memory card to expandstorage of machines setup*.
Programmable computer unit:
High efficiency and easy-to-use display
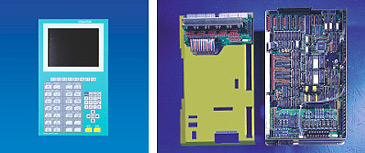
10" color screen (option)
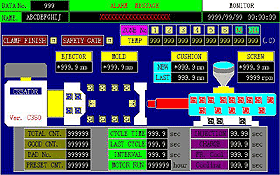
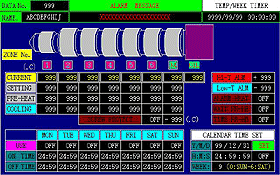
- The computer controller, made in Japan with LCD display, is easy to use, operate, andset.
- It is quick and simple to call up the program to the LCD display for modification.
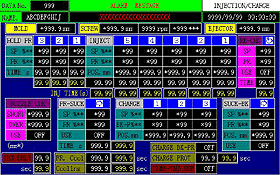 |
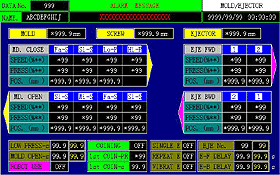 |
Injection/charge setting apge |
Injection/charge setting apge |
 |
 |
Machine status page |
Temperature setting page |
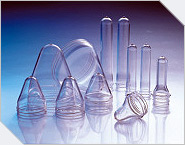
High-speed cycle can produce very thin-shelled products.
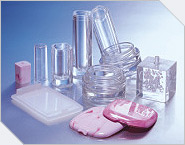
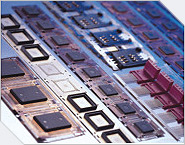
Holding evenly with perfectly parallel platen.
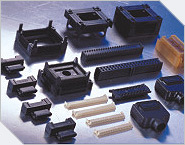
High plasticizing and good hold pressure.
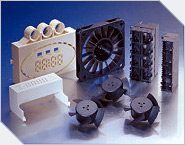
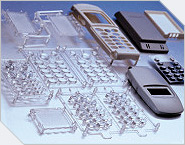
High speed Thin-wall products.
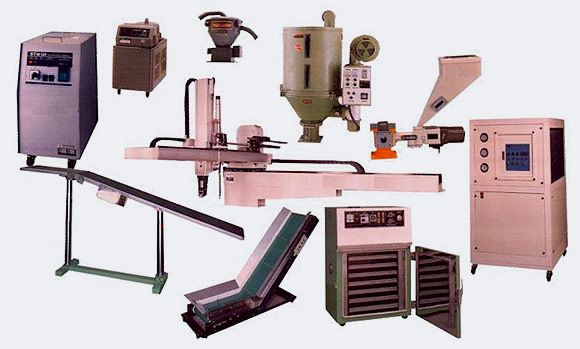
We can offer, you the customer, a wide range of accessories to complement your injection machine.
These accessories are available locally and are manufactured to the highest quality.
Please see below for what we can supply.
(Please Note: These accessories are not sold separately, only with a Creator Machine)
- Auto Loaders
- Hopper Dryers
- Dust Collectors
- Robots
- Moulds
- Granulators
- Conveyors
- Chillers
- Dehumidifiers
- Mould Temperature Controllers
- Oven Dryers
- Masterbatch